From field to PLC
Every input.
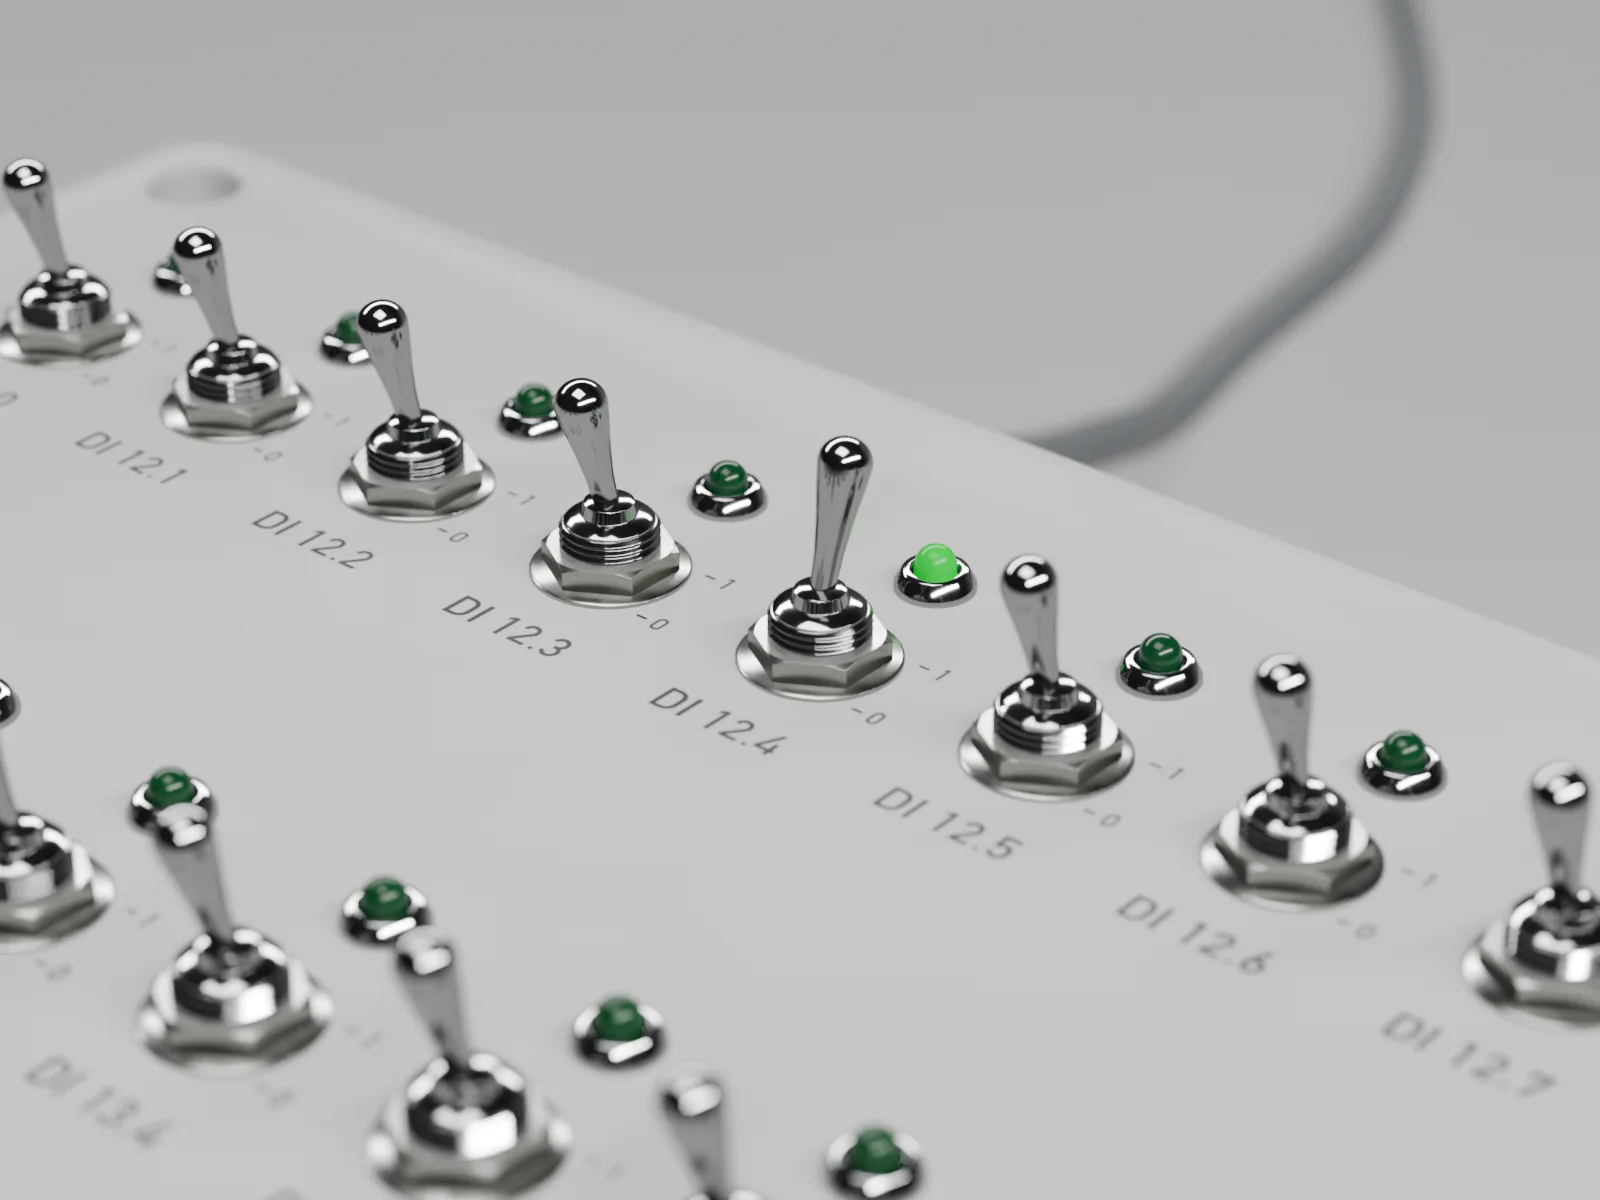
A toggle switch stands in for the sensor. If the bit doesn’t move, the problem is somewhere between cable, terminal and power supply.
14 open
A sample punch list, in the format we keep on site · not data from a real job
Testing and start-up · since 1996
Anything that doesn’t check out gets its own row: what’s wrong, how much it matters, who closes it. The line goes live when that list hits zero, not when the date comes around.
Technical reply in 1–2 business days · No commitment
Scroll: watch the list empty
Companies that have trusted us
FAT and SAT
In our workshop we test everything that can be tested without the process. At your plant, all that’s left is what only the process can tell us.
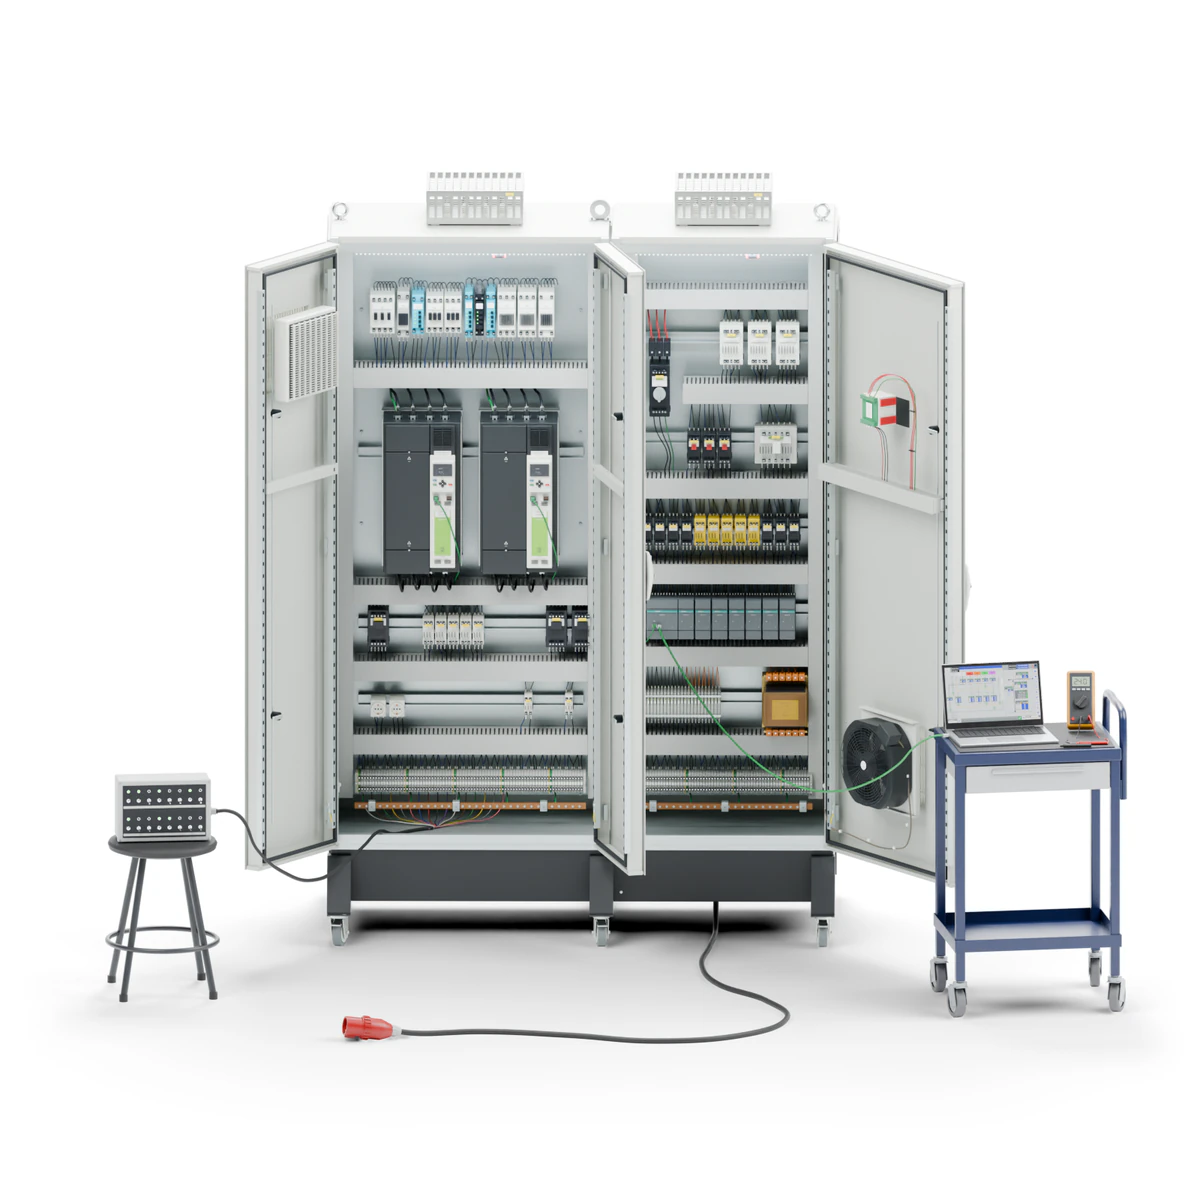
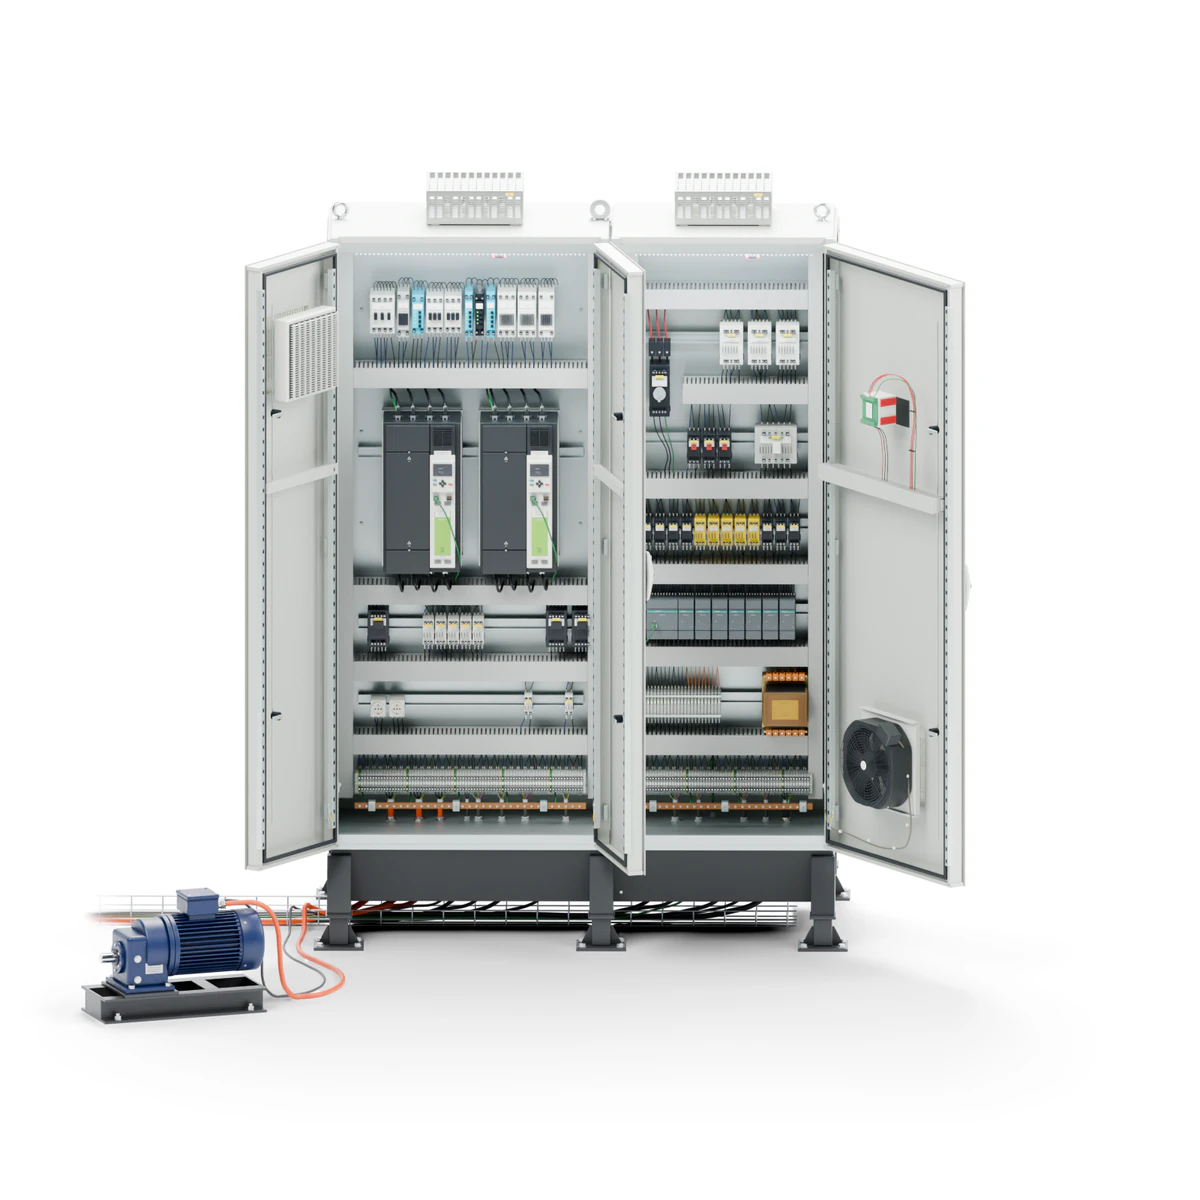
FAT saves you days.
SAT saves you downtime.
Testing
An input can be inverted, an analog signal off scale, a drive enabled with no feedback. On the test bench that’s ten minutes; on site it’s hours.
Each square is one signal
336 of 336 tested
Force the field device, watch the PLC. If the bit doesn’t change, the problem isn’t in the software.
DI 12.4 infeed photocell. Expected 1, read 0. The signal comes in inverted.
DI 12.4 fixed at the terminal block. Retested, closed. On site it would have been two hours and a stopped line.
336 tested, 336 passed. Now we can talk about start-up.
From field to PLC
A toggle switch stands in for the sensor. If the bit doesn’t move, the problem is somewhere between cable, terminal and power supply.

From PLC to field
We drive it from the PLC and measure at the terminal. The right thing has to move: that contactor, that valve, that lamp. Not the one next to it.
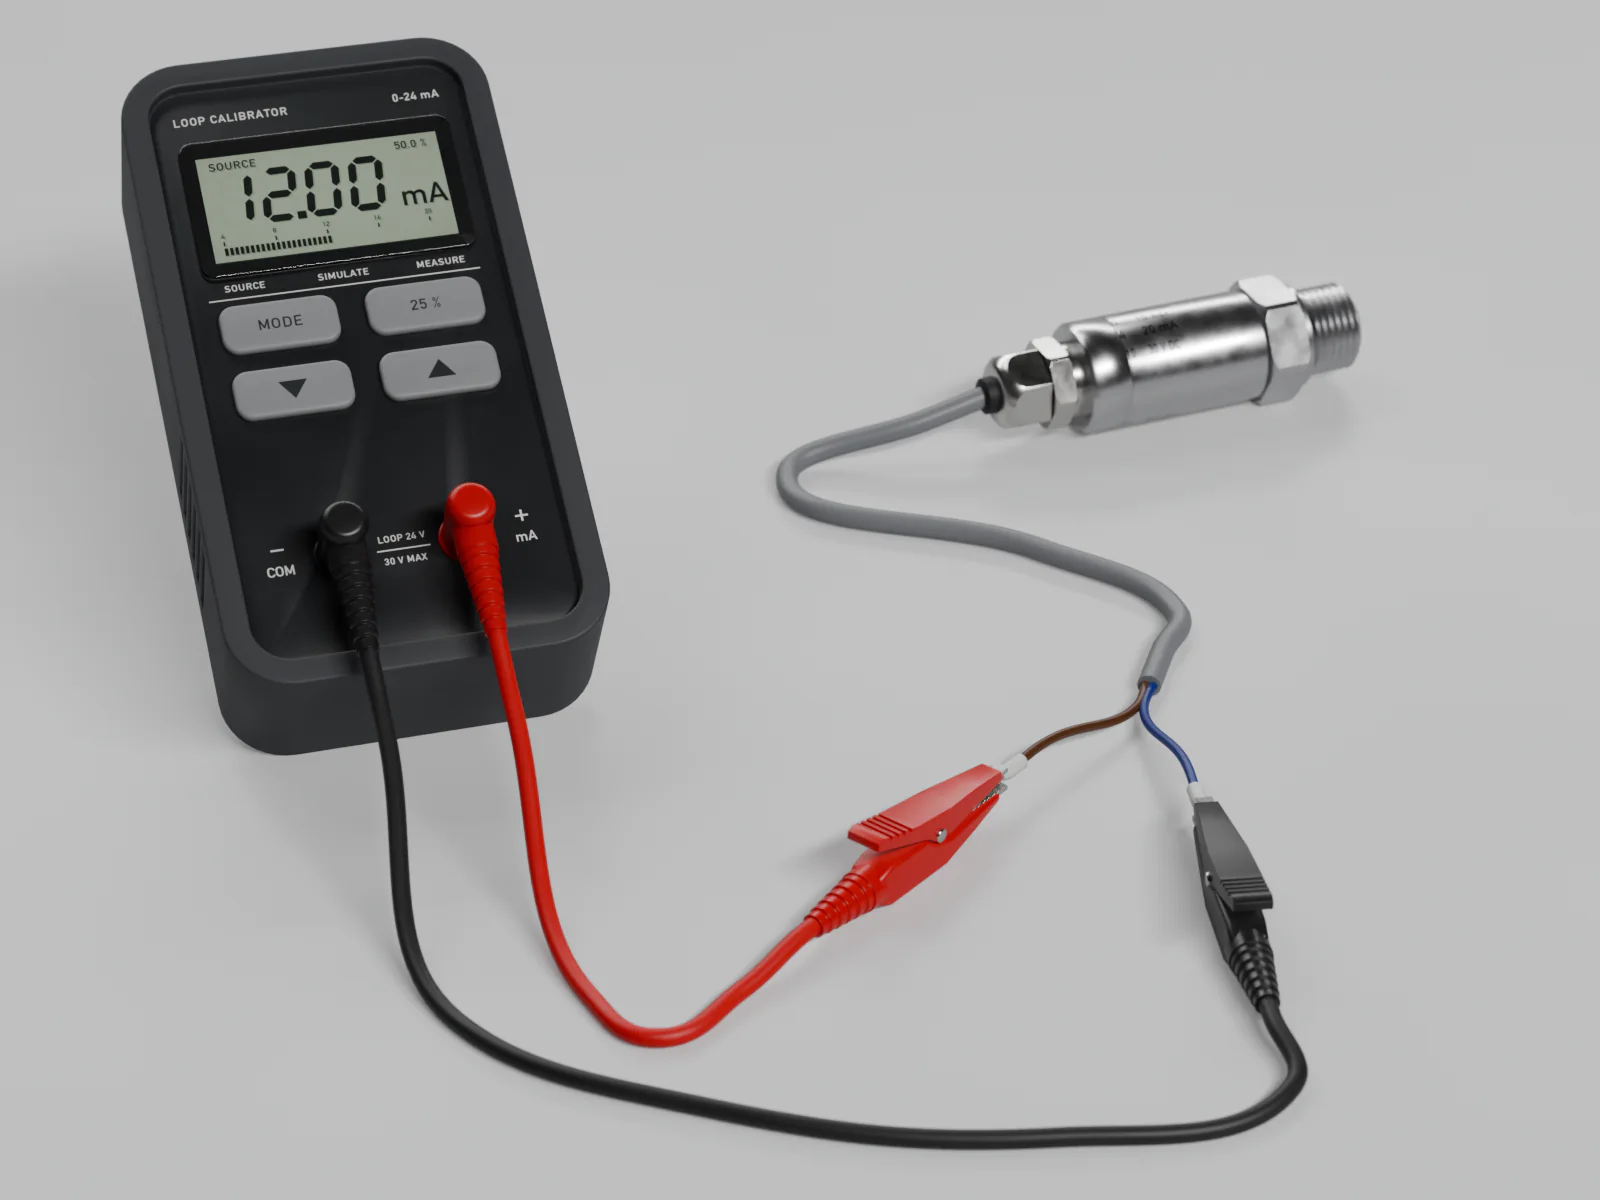
With the instrument
Zero and full scale. A badly scaled 4–20 mA signal goes unnoticed until it ruins product, and by then it’s scrap.
Start-up
A machine can dry-cycle perfectly and stop at the first changeover. Start-up is over when the line makes product, at the right rate, run by the people who use it every day.

Until material goes
through, the cycle
is still a guess.
Real product exposes what an empty run never will: tension, temperatures, settling times, start‑up scrap.
8 hours
straight.
A single cycle almost always works. Eight hours straight is another story: that’s when overloads trip, timings run at the limit, false alarms show up and parts pile up where nobody was looking.
A line only two
people can run
stops with those two.
We walk the people on shift through it, not just whoever followed the project.
Service
The part that isn’t in the quote: what happens the day after the acceptance report is signed.
The first hours
We watch them with you: that’s when the last issues surface.
The first year
Call whenever you need to, without wondering what the question will cost.
Always
For anyone who has bought from us, every day.
If the plant has secure, authorized remote access, we run most post-start-up checks from Mesero, without waiting for a trip. How our remote support works
Handover
Not a binder to file away: the things you need the first time the line stops and we’re not there.
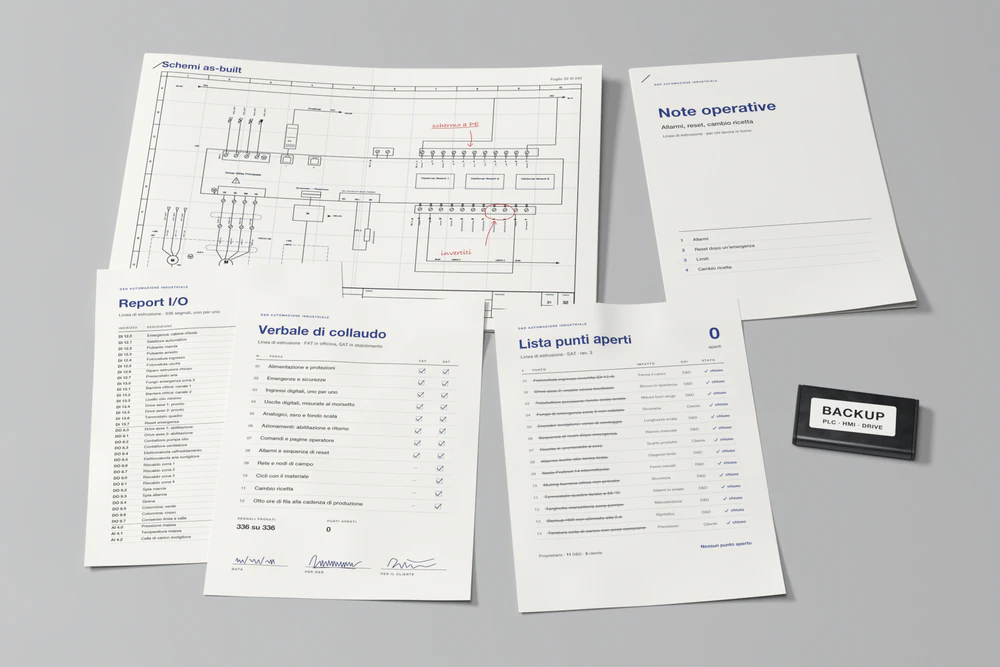
What was tested, with the result, the date and the signature of whoever was there.
Every signal, its address, the expected value and the value read.
Closed items, with the date and who closed them. Yours included.
PLC, HMI, drives and parameters: the version left in the machine, with the date on it.
Alarms, resets, limits, recipe changes: what the people on shift need to know.
Updated with the changes made on site, not the ones we started from.
Everything in formats you can still open ten years from now, without calling us to do it. When a change is ours, we redraw the schematics ourselves: see how we draw them.
First step
Tell us when the line has to produce and what needs testing. We’ll tell you what’s worth testing on the bench, what can only be tested on site, and how many days it really takes.
An engineer reads it, and the first reply comes within 1–2 business days.
Already in start-up and the line is down? Call +39 02 97289083: that’s when it pays to skip the form. Or email info@dedautomazione.it.